

Hot stamping puts a permanent mark on a part without ink systems, cure time, or solvent cleanup. The die material you pick decides most of what happens after that. Magnesium is cut fast and cheap for short runs and prototypes. Brass holds fine detail through medium volumes on leather, paper, and softer plastics. Steel goes into long production runs and hard engineered plastics, where a higher price up front drops the cost per impression over the life of the die. Here is how to tell which one your job calls for.
How does a hot stamping press make a permanent mark?
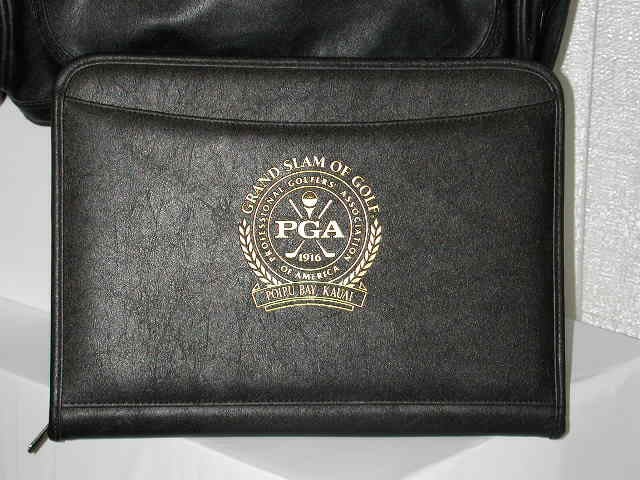
A hot stamping press heats a metal die or type, drives it against a strip of hot stamping foil laid over the part, and transfers pigment from the foil carrier onto the surface. The press lifts away and the mark is complete, permanent and dry, with no cure step. Run the same die without foil and the heated face burns the image directly into the material.
The cycle is short and it repeats identically. Load the die, set the foil, fixture the part, make the mark. Nothing about that sequence changes between a hand-fed bench press in a leather shop and an inline printer coding pouches at line speed. That repeatability is why the process has held its ground for more than a century while newer marking methods have come and gone.
Everything downstream depends on the die face. The image is engraved from your artwork, so the file you supply sets the ceiling on detail. Adobe Illustrator files work best, and DWG, DXF, and EPS all work. Durable Technologies engraves die faces from supplied graphics files and will tell you before cutting whether a piece of artwork will hold at the size you need.
What materials are hot stamping dies made from?
Hot stamping dies are made from magnesium, brass, or hardened tool steel. Magnesium is the softest and least expensive, etched quickly for short runs and prototypes. Brass sits in the middle and holds fine detail through medium production volumes on most soft substrates. Steel is the hardest and longest-lived, built for high volumes and for marking hard engineered plastics.
The ladder is straightforward: harder material, longer die life, higher price, longer lead time. Where operators get burned is at the two ends. Buying magnesium for a job that will run all year means re-ordering new dies every few months and living with a mark that drifts. Buying steel for a 500-piece seasonal promotion means paying for die life nobody will ever use.
Softer alloys show up in the market too. Zinc and lead type is cheaper than brass and wears faster under heat and pressure, and the mark it leaves is noticeably less crisp from the first impression forward. Brass outwears both.
Mounting matters as much as the alloy on shorter jobs. Dies come mounted or unmounted at industry-standard type heights, so a shop running several presses can move a die between machines without re-fixturing the whole setup.
When should you choose brass hot stamping dies?
Brass hot stamping dies are the right call for medium production volumes where the mark has to look good, not just be legible. Brass holds fine serifs and small logo detail, outwears softer zinc and lead alloys under heat and pressure, and marks books and book bindings, leather goods, most plastics, paper products, and wood. It costs less than steel and lasts far longer than magnesium.
Finish quality is the reason most personalization and luxury goods work runs on brass. When the stamped logo is part of what the customer is paying for, a die that softens after a few thousand impressions becomes a quality problem.
Royce Leather Gifts in Secaucus, NJ has been making custom leather goods since 1974 and runs brass dies from Durable Technologies' VisiMark division on their Kwikprint machines. Managing Director William Bauer put a number on it: "We run 40,000 plus passport cases per year, and the last stamped impression is the same excellent quality as the first one." That is the range brass was made for. Volume high enough that magnesium would give out, substrate controlled enough that steel is not required.
The tradeoff is real. On glass-filled nylon or a similarly hard engineered plastic, a brass die will deform before it wears out. Substrate hardness, not just piece count, is what pushes a job to steel.
Durable Technologies manufactures brass type and logo dies, printers' type, monogramming type, and Kingsley® wire marking type from its VisiMark operation in Worcester, MA.
When is a steel hot stamping die worth the cost?
A steel hot stamping die pays for itself when the run is long, the substrate is hard, or both. Hardened and tempered tool steel holds its engraved detail through production volumes that would flatten brass, and it marks harder plastics that soften brass die faces. Higher price up front, lower cost per impression across the life of the die, and fewer replacement orders to manage.
Do the math on impressions rather than on the purchase order. A die that costs more and produces several times the number of impressions before needing to be replaced is the "more valuable" die, and it also removes the changeover time and scrap that come with swapping in a fresh one mid-program. For a shop coding the same part number year after year, that stability is worth more than the price difference.
Steel earns its place in industrial marking for the same reason it does in packaging. Steel hot stamping dies hold up in continuous operation and keep producing the same legible mark on the ten-thousandth part as on the first, which is what audit trails and traceability requirements demand.
Steel is the wrong answer for a short run or a design still in revision. Lead time is longer and the die cost is not recovered on a few hundred pieces. Prove the artwork first, then commit to steel when the design stops changing.
What jobs are magnesium hot stamping dies best for?
Magnesium dies are the low-cost, fast-turnaround option for short production runs, prototypes, and artwork that changes often. They are etched quickly, priced well below brass, and run across a wide range of imprinting machines. Substrates include plastics, leather, wood, and paper products, and dies ship mounted or unmounted at industry-standard heights.
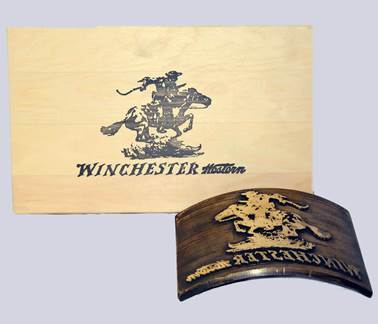
Speed is the point. When a customer approves artwork on Tuesday and needs stamped samples by Friday, magnesium is the only material that gets there. It is also the sensible way to test a new logo at production settings before committing to a brass or steel cut, because finding a detail problem on a cheap die is a lot better than finding it on an expensive one.
The commercial printing and specialty trades run on magnesium for exactly this reason. Greeting cards, labels, book bindings, matchbooks, ribbons and bows, advertising specialties, letterpress work, jewelry boxes, menu covers, and napkins are all short-cycle, high-variety jobs where the die changes more often than the press does.
Magnesium wears faster than brass, and on a long run the mark degrades gradually rather than failing outright, which makes it easy to miss until a quality check catches it. Watch impression counts on any magnesium die that gets pulled back into repeat production.
Which die material is right for your production run?
Match the die material to run length first and substrate hardness second. Magnesium for short runs, prototypes, and frequently changing artwork. Brass for medium volumes on leather, paper, wood, and soft plastics where finish quality matters. Steel for long runs and hard engineered plastics. Budget is the third input, and it should be evaluated as cost per impression rather than die price.
| Magnesium | Brass | Steel | |
|---|---|---|---|
| Typical run length | Short runs and prototypes | Medium production volumes | High volume, continuous |
| Best substrates | Paper, card stock, leather, wood, soft plastics | Leather, books and bindings, paper, wood, most plastics | Hard and engineered plastics |
| Detail retention | Good when new, softens with use | Crisp and stable through the run | Holds detail longest under load |
| Relative die cost | Lowest | Moderate | Highest |
| Cost per impression at volume | Highest | Low | Lowest |
| Lead time | Fastest | Moderate | Longest |
| Typical buyer | Printers, specialty shops, anyone proving artwork | Leather goods, personalization, book binding | Packaging lines, industrial part marking |
Two questions settle most of these decisions. How many impressions before the artwork changes, and how hard is the material being stamped. Answer those questions honestly and the material picks itself. Buyers get it wrong by estimating volume from the current purchase order when they should be estimating from the program. That is how a die meant to last a quarter ends up running for three years.
Durable Technologies makes a die material recommendation based on mark depth, expected impression count, budget, and how the press is operated. That last input gets overlooked. An operator running a manual press at inconsistent dwell will wear any die faster than a timed inline unit will.
Hot stamping dies from Durable Technologies include brass and steel type and logo dies, printers' type, monogramming type, Kingsley® wire marking type, heat shrink sleeving type, type holders, magnesium dies, and branding iron dies.
Which industries use hot stamping dies most often?
Hot stamping dies show up wherever a permanent, legible mark has to go on a non-metal surface. Pharmaceutical and food packaging use them for date and lot coding. Wire and cable shops use them for conductor marking and heat shrink sleeving. Leather goods, cosmetics packaging, book binding, and promotional products use them for branded impressions.
Packaging is the highest-volume application. Pigmented foils imprint variable data such as production dates, expiration dates, and storage life onto packaging films, plastics, and coated and uncoated label stocks. Pharmaceutical package marking is the demanding end of that work, because the code has to stay legible through distribution and it has to be right every single time.
Wire marking runs on foil chemistry as much as on die material. Durable Technologies supplies the No Fault Series formulated for cross-linked polyolefin heat shrink sleeving, which has also proven out on PVC, Kynar, Neoprene, and other cross-linked materials with good abrasion and solvent resistance.
Branding irons cover the industrial end. A heated die burns a trademark, certification, or plant code into cork, chamois, leather, plastics, paper, rubber, wood, particle board, and wallboard. PVC pipe gets branded this way so a length that shows up on a job site can be traced back to the manufacturer and its certifications.
If you want to see how our hot stamping dies helped a long-time customer deliver legible and consistent pharmaceutical package marking, read the testimonial Hot Stamping Coding Type for Pharmaceutical Packaging.
Frequently asked questions about hot stamping dies
How long does a hot stamping die last?
Die life depends on material, substrate, and press settings more than on any published number. Magnesium is measured in short runs, brass carries medium production volumes, and hardened tool steel runs longest. Substrate hardness and operator dwell time both shorten die life significantly, so two shops running the same die can see very different results.
Can you hot stamp without using foil?
Yes. Running a heated die without foil burns the image directly into the material, which is how branding irons work on wood, leather, cork, rubber, and PVC pipe. The mark comes out as a debossed burn rather than a colored impression. Foil is only needed when you want pigment and color in the finished mark.
What is the difference between hot stamping type and a logo die?
Type is a set of interchangeable characters loaded into a holder, so the copy can be changed between runs for dates, lot codes, or names. A logo die is a single solid engraved plate carrying fixed artwork. Choose type when the copy varies and a logo die when the same image repeats on every part.
Are magnesium dies strong enough for real production?
Magnesium handles genuine production work, just in shorter cycles. It is well suited to runs measured in hundreds or low thousands, to prototypes, and to artwork that changes seasonally. Problems appear when a magnesium die intended for a short run gets pulled back into repeat production, where the mark degrades gradually and quietly.
Should I use brass or steel dies for plastic parts?
It depends on which plastic. Brass handles softer plastics well and produces a crisper mark than cheaper alloys. Hard and engineered plastics will deform a brass die face over time, and those applications call for hardened tool steel. We can help with this recommendation.
What artwork format do you need to make a custom die?
Adobe Illustrator files are preferred, and DWG, DXF, and EPS files all work. The engraved image is created from the graphics file you supply, so line weight and detail in the artwork set the limit on what the die face can hold. Send artwork at the finished stamping size whenever possible.
Can hot stamping dies mark metal parts?
No. Hot stamping is for non-metal surfaces such as plastics, leather, paper, wood, rubber, and fabric. Marking metal calls for a different process, typically steel hand stamps, roll marking dies, dot peen, or a marking press. Durable Technologies supplies tooling for both, so the same conversation can cover a mixed part list.
Tell us the substrate, the annual volume, and how the mark gets used downstream, and we will recommend the die material that fits. Call 866-344-7721 or contact us to request a quote.